Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Precision cold-rolled stainless steel strip, coil and belt solutions
Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
A practical comparison of 301 full-hard and extra-hard strip, including where additional strength helps and where it creates forming and fatigue risk.

301 full hard strip and extra-hard strip both sit at the high-strength end of the cold-rolled family, but they should not be treated as interchangeable catalogue labels. The acceptance range, forming allowance and edge sensitivity must be linked to the finished part.
Extra-hard material usually represents an additional cold-reduction or temper target beyond a supplier’s full-hard range. The exact range depends on thickness, chemistry and the agreed standard.
Ask for yield strength, tensile strength, elongation and hardness together. A higher minimum tensile value is not useful if the corresponding maximum and test method are left undefined.
Extra hardness may help a part resist permanent set or increase contact force, but it can also amplify springback and reduce the bend radius that remains crack-free.
| Requirement | Full-hard focus | Extra-hard focus |
|---|---|---|
| Strength | High strength with a broader forming margin | Maximum strength family |
| Springback | Still significant; tool compensation required | Usually more sensitive to tool and thickness variation |
| Edge quality | Burr control is important | Burr and microcrack control are critical |
| Forming trial | Recommended | Essential for a new geometry |
A small gauge change has a larger relative effect when the strip is very thin. It changes section stiffness and can shift springback outside the tool’s adjustment range.
Define thickness tolerance by measurement location and method. Include flatness, camber and edge condition because the press responds to the delivered strip, not to a single table value.
HIQ can discuss 301 full-hard and extra-hard requirements around the forming operation, annual volume and required width. The production route includes controlled cold rolling, annealing, tempering, levelling and slitting.
A China-based integrated supplier is most valuable at this stage: engineering, rolling and slitting teams can review the same drawing instead of passing a tolerance problem through several unrelated processors.
If the risk is breakage, trial the smallest production bend radius. If the risk is poor contact force, measure load after formation and after a defined hold period. If the risk is dimensional, check parts from multiple coil positions.
This application-led approval is more reliable than selecting the hardest strip available and attempting to tune the tool afterwards.

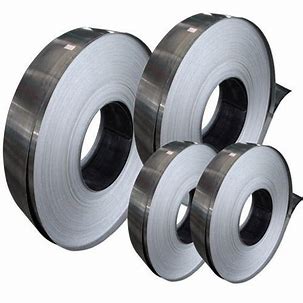
It can be formed in suitable geometries, but the bend radius, grain direction and edge quality must be validated for the specific temper and thickness.
It can increase slitting, handling and forming sensitivity. The real cost should include yield loss and trial iterations, not only material price.
That depends on the route and property targets. Discuss the complete sequence before slitting so the final mechanical state is not changed unintentionally.
Before you approve 301 full hard strip, send the drawing, grade or application, target thickness and width, temper, surface, edge requirement, operating environment and estimated annual volume. Our Shanghai and Danyang teams will review the manufacturing route and identify the details that should be tested before production.
Related HIQ resources: 301 stainless strip product · Temper selection guide · Request a forming review · World Stainless Association technical resources
